Inspection and diagnostics of turbines and compressors
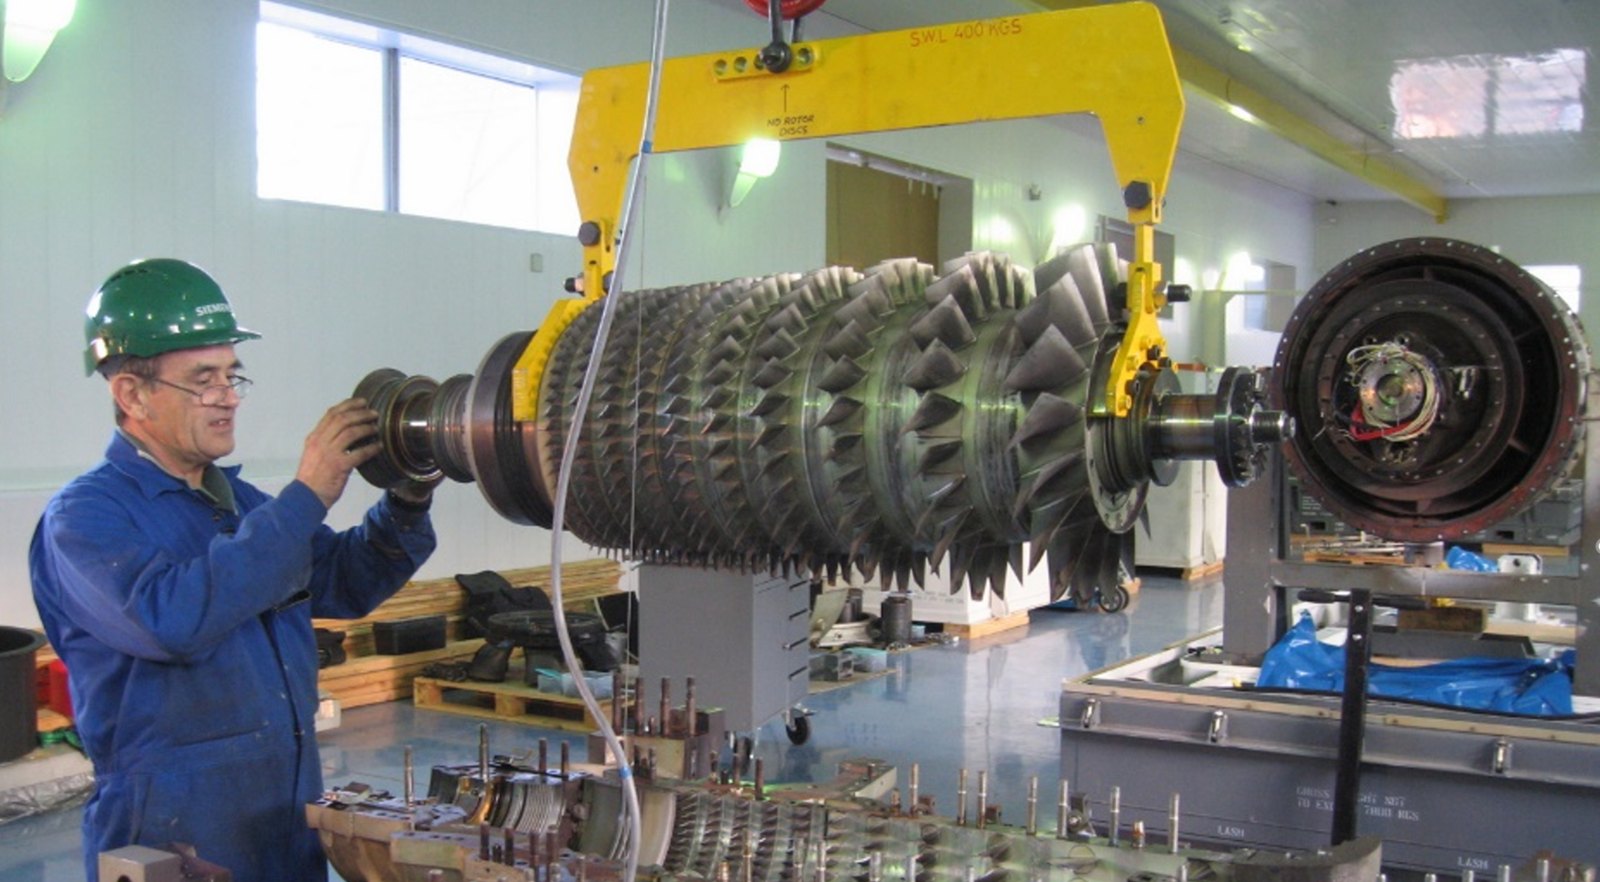
A diagnostic survey assesses the current condition of a turbine or compressor and of its spare parts and forecasts the maintenance ahead. We carry it out before installation, commissioning or maintenance, perform minor inspections by running hours and advise in abnormal situations. Equipment rated 750 kW – 80 MW; our specialists were trained at the manufacturers' plants.
Scope
- diagnostic survey of the machine and its auxiliary systems: oil system, seals, instrumentation and controls
- assessment of the condition and completeness of the spare parts held by the customer
- forecast of the maintenance ahead and a list of the parts required
- survey before installation, commissioning or maintenance
- minor inspections by running hours: examination of the hot section and auxiliaries without dismantling
- analysis of data from the vibration monitoring and control systems
- advice in abnormal situations
- a technical report with recommendations for further operation
Types of inspection and survey
The type of inspection depends on the task: assessing condition before installation or repair, checking a machine by running hours, or investigating an abnormal event. The scope and intervals of scheduled inspections are set by the manufacturer’s operating manual; unscheduled inspections are triggered by an event or by diagnostic findings. Inspection level names and their scope differ between manufacturers, so the table shows generalised types of work.
| Type | When | What is done | Machine shutdown |
|---|---|---|---|
| Diagnostic survey | on request; before installation, commissioning or maintenance work begins | the machine and spare parts are assessed, completeness is checked and the scope of maintenance ahead is forecast | data analysis with the machine running, examination with the machine stopped |
| Minor inspection | by running hours; the scope is set by the operating manual | the machine and auxiliaries are examined without dismantling; on a gas turbine, the hot section as well | required |
| Gas turbine inspections with opening-up: combustion, hot gas path, major | by equivalent running hours, to the manufacturer’s schedule | partial or complete dismantling, defect assessment, replacement of worn parts | extended, planned together with a repair |
| Advice in an abnormal situation | after a protection trip or a rise in vibration or temperatures | event logs and trends are analysed and recommendations are given on further operation | decided on the basis of the analysis |
Work that involves opening up the machine is planned as a repair: medium and major overhauls of gas turbines are described on the gas turbine service and repair page.
Inspection before installation and after long-term storage
If a machine has waited a long time for installation in a warehouse or on site, it is checked for condition and completeness before installation. A preservation defect or a missing part is cheaper to find before installation than during commissioning. Inspection of previously supplied equipment, diagnostics of system condition and completeness checks are among the company’s services.
What is checked
- completeness against the packing lists and the scope of supply, and availability of the manufacturer’s documentation;
- the state of preservation: protective coatings, nozzle blanking covers, desiccant, and inert gas overpressure where the casing has been filled with it;
- signs of corrosion, damage in transit and storage, and the condition of the packaging;
- compliance with the manufacturer’s storage requirements, checked against the log: conditions, periodic rotor turning, re-preservation;
- spare parts and consumables in store: shelf life, packaging and match to the machine.
The report lists findings and missing items and recommends where re-preservation is sufficient and where components need to be opened and checked before installation. Receiving, storage and preservation of machinery before commissioning are covered, for example, by API RP 686; for a specific machine, its manufacturer’s requirements apply. The next stage is installation supervision and commissioning.
How the survey proceeds
- 1
Request and data
Model, serial number, running hours, event logs and the concern.
- 2
Survey
Examination on site or analysis of the customer's data; measurements without dismantling.
- 3
Analysis
Comparison with the manufacturer's documentation and the operating history.
- 4
Report and recommendations
Machine condition, maintenance forecast, list of parts and work.
Borescope inspection: what can be seen without opening up
A borescope is a rigid or flexible optical probe, usually fitted with a video camera. It is inserted into the gas path through dedicated ports in the casing to examine blades, combustion liners and other parts without removing the casing covers. Under GOST R EN 13018-2014 this is visual testing: it shows the condition of surfaces but does not replace measurements and non-destructive testing during a repair. The machine is shut down and cooled before the inspection.
| Section | What is looked for |
|---|---|
| Compressor | fouling and erosion of blades, leading-edge nicks from foreign objects, signs of blade tips rubbing against the casing |
| Combustor | cracks and burn-through of combustion liners, spalling of the thermal barrier coating, damage to burners and transition pieces |
| Turbine | oxidation, corrosion and coating loss on first-stage vanes and blades, cracks, nicks from fragments of combustor parts |
The main value of borescope inspection lies in comparison. Images taken from the same positions as at the previous inspection show how fast wear is progressing. They are used to decide whether the machine can run until the planned repair and to order in advance the parts that will need replacing. Crack depth and the condition of parts beyond the probe’s reach can only be assessed when the machine is opened up.
Which data help assess condition
A single measurement says little about a machine, so the analysis needs its operating history. A slow rise in vibration or bearing temperature points to a developing defect; a sudden step change points to an event after which the machine should be examined. Condition monitoring programmes under GOST R ISO 17359-2015 are built on the same parameters.
- running hours and number of starts; for a gas turbine, also operation at peak load and on liquid fuel, which are used to calculate equivalent running hours;
- event logs: protection trips, emergency shutdowns, compressor surge;
- trends of vibration, bearing and exhaust gas temperatures, and oil and seal gas pressures;
- oil analysis results: cleanliness code to ISO 4406 and water content;
- reports and photographs from previous inspections and repairs, and a list of replaced parts.
If the vibration trends call for separate work — measurements across operating modes, balancing, alignment — it is carried out as part of vibration diagnostics and field balancing.
Inspection report and repair plan
The report answers three questions: what condition the machine is in, how long it can run before a repair, and what needs to be prepared for it. This sequence — detecting a deviation, identifying its cause, making a prognosis and giving recommendations — follows the approach of GOST R ISO 13381-1-2016 to machine condition prognostics.
| Finding | Recommendation |
|---|---|
| Condition within the manufacturer’s limits | operation until the scheduled date, check at the next inspection |
| Progressing wear | more frequent monitoring, parts ordered for the next repair |
| Defect beyond the permissible limit | restricted operation or shutdown, and repair to an agreed programme |
The parts list from the report is checked against the customer’s stock so that the repair does not wait for deliveries. Missing items can be ordered in the spare parts section. A report on the actual condition also serves as justification if a scheduled inspection is postponed within the limits allowed by the manufacturer.
Why customers choose us
- 1
End-to-end approach
From diagnostics and the repair plan through to handover into operation.
- 2
Qualified engineers
Our specialists were trained at the turbine and compressor manufacturers' plants.
- 3
Original parts
We confirm the origin of parts by catalogue numbers, markings and accompanying documents.
- 4
Energy Management LLC warranty
Warranty cases on work and spare parts are handled by our own specialists.
Example: inspection of Siemens STC-SV turbocompressors
In July 2023, the company’s specialists carried out a scheduled Level 1 inspection of two Siemens STC-SV (08-7-A) turbocompressors at the facilities of the Gazprom Pererabotka condensate treatment plant (ZPKT). The inspection was part of the TR-6000 scheduled repair and was performed under a works contract dated 28 March 2023.
The STC-SV is a single-shaft centrifugal compressor with a vertically split casing. According to the manufacturer, all of the compressor’s internals are assembled into a single bundle, which is withdrawn axially from the casing without disconnecting the process piping. Service for this range is described on the Siemens Energy SST steam turbine and STC compressor service page.
In its letter of 6 October 2023, GSP Remont LLC stated: “The work was carried out in accordance with the requirements of the regulatory and technical documentation, at a high organisational and technical level and within the time frame set by the contract” (translated from Russian). The scan of the letter is in the customer letters of appreciation section.
Manufacturer names and designations are given to identify the equipment we service. Trademarks belong to their respective owners.
Causes of failure and recommendations
Why turbines and compressors fail
- operation outside the rules
- unsuitable components
- excessive vibration
- foundation defects or the influence of adjacent equipment
- late replacement of wearing parts
- end of service life
How to extend service life
- regular diagnostics and maintenance
- consumables and parts specified by the manufacturer
- qualified specialists
Projects and related pages
Questions and answers
How does a diagnostic survey differ from a minor inspection?
A diagnostic survey assesses the condition of the machine and its <a class="term-link" href="../glossary/spare-parts/index.html" title="What spare parts are and how their origin is confirmed">spare parts</a> and forecasts maintenance; it is carried out on request, before installation, commissioning or repair. A minor inspection is performed by running hours to the scope of the operating manual: examination of the hot section and auxiliaries without dismantling.
Does the equipment have to be shut down?
Some measurements and the analysis of vibration monitoring data are done with the machine running; examination of the hot section requires a shutdown. The scope is agreed with the customer in advance.
How quickly does an engineer travel to site?
Response and call-out times are agreed with the customer for each request and kept as short as possible.
What can a borescope inspection of a gas turbine reveal?
The borescope is inserted through dedicated casing ports to examine the gas path without removing the covers. In the compressor, it reveals fouling, erosion and nicks on blades; in the combustor, cracks and burn-through of liners and spalling of the thermal barrier coating; in the turbine, oxidation and damage to first-stage vanes and blades. Crack depth and parts beyond the probe’s reach can only be assessed when the machine is opened up.
Do you inspect equipment that has been in storage for a long time before installation?
Yes. Inspection of previously supplied equipment and completeness checks are among the company’s services. Such an inspection covers completeness against the packing lists, the state of preservation, signs of corrosion and damage, compliance with the manufacturer’s storage requirements, and the spare parts in store. The result is a list of findings with recommendations on where re-preservation is enough and where components need to be opened and checked before installation.
Engineering team
Gas turbine service